GH25 vs GP25: What Is the Difference and Can You Mix These Steel Grit Grades
GH25 and GP25 are the two most widely used grades of high-carbon cast steel grit for blast cleaning of metal surfaces. Both share the same G25 size and an almost identical chemical composition, so customers often ask whether they can be loaded into one hopper and whether there is any real difference between them. In this article, the Ingritech team compares GH25 and GP25 in terms of hardness, particle shape and application, explains what ISO and SAE standards say about mixing abrasives, and gives practical recommendations for companies selecting blast media for their equipment.
What Are GH25 and GP25
GH25 and GP25 are grades of high-carbon cast steel grit (angular abrasive) produced by crushing cast steel shot. Their chemical composition is practically the same: carbon approx. 0.80–1.20%, manganese 0.60–1.20%, silicon from 0.40%, sulphur and phosphorus max. 0.05% each. Both grades have a density of approx. 7.3–7.6 g/cm³ and a bulk density of approx. 4.2 g/cm³. They are cast high-carbon abrasives with a martensitic structure and fine carbides, which protects the particles from premature breakdown.
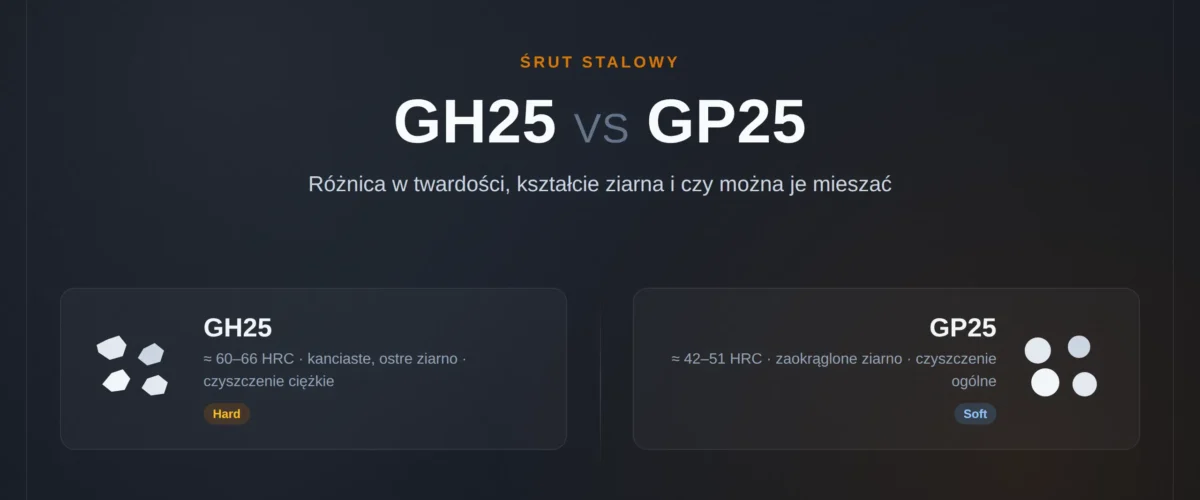
The key difference between GH25 and GP25 lies in hardness and in how the particle behaves during operation:
- GH25 (Hard) – maximum hardness, approx. 60–66 HRC (≈ 620–720 HV). The particles are angular and sharp and, importantly, stay angular throughout their service life. This grit is designed for heavy-duty work: deep cleaning, removal of heavy mill scale and creating a coarse surface profile, e.g. in wheel blast (turbine) machines.
- GP25 (Soft) – a softer grade, approx. 42–51 HRC (≈ 470–550 HV). The particles are also angular at first but round off quickly in use. GP25 works well for general surface cleaning: removing rust and scale and producing a moderate profile without excessive damage to the base material.
GH25 vs GP25 Comparison Table
| Parameter | GH25 | GP25 |
|---|---|---|
| Material type | High-carbon cast steel grit | High-carbon cast steel grit |
| Chemical composition | C 0.80–1.20%, Mn 0.60–1.20%, Si ≥ 0.40%, S, P ≤ 0.05% | C 0.80–1.20%, Mn 0.60–1.20%, Si ≥ 0.40%, S, P ≤ 0.05% |
| Hardness | ≈ 60–66 HRC (620–720 HV) | ≈ 42–51 HRC (470–550 HV) |
| Density | ≈ 7.3–7.6 g/cm³ | ≈ 7.3–7.6 g/cm³ |
| Particle shape | Angular, sharp; stays sharp in use | Angular at first, rounds off quickly |
| Size | G25 (≈ 0.8–1.2 mm) | G25 (≈ 0.8–1.2 mm), same size |
| Bulk density | ≈ 4.2 g/cm³ | ≈ 4.2 g/cm³ |
| Brittleness | High hardness → more brittle on impact | Lower hardness → higher toughness |
| Application | Heavy-duty work: deep cleaning, coarse profile, wheel blast (turbine) machines | General cleaning: rust and scale removal, moderate profile |
Which Standards Cover Steel Grit
Several international standards define the size, hardness and permitted contaminants of blast cleaning abrasives. None of them, however, explicitly prohibits or regulates mixing different grades in one hopper:
- ISO 11124-3:2018 – the international standard for high-carbon cast steel shot and grit. It defines the abrasive designation (e.g. M/HCS/G025/…HV), size and Vickers hardness requirements, and the concept of “foreign matter”, i.e. non-magnetic particles. Since both GH25 and GP25 are ferrous (magnetic) materials, they do not fall under the foreign-matter limits, which apply to contaminants such as sand or slag.
- SAE J1993 – the US specification “High-Carbon Cast-Steel Grit”, which details chemical composition and hardness ranges for each class: GP (soft), GL (medium) and GH (hard, from approx. 60 HRC). The standard does not require GH and GP to be stored separately, but strictly controls the hardness and cleanliness of the abrasive.
- SAE J444 – the size (grading) standard for blast cleaning abrasives; it is this standard that defines G25 as a nominal particle size of approx. 0.8–1.2 mm.
- ISO 11125 (series) – test methods for metallic abrasives: sampling (ISO 11125-1), particle size distribution (ISO 11125-2), hardness (ISO 11125-3), etc.
All of these standards describe the properties of a single, individual abrasive. Neither ISO nor SAE gives any specific guidance on mixing GH25 with GP25. All sources agree on one point, though: abrasives must be stored dry, because moisture causes particle corrosion and dust build-up, which reduces both safety and blasting quality.
Can GH25 and GP25 Be Mixed in One Hopper
Formally, mixing GH25 and GP25 is possible: both materials are magnetic and meet ISO 11124-3 and SAE J1993 requirements for high-carbon abrasives. Technically, however, it involves a number of risks, and mixing is not recommended without thorough prior testing. The main technical risks:
- Hopper and feeder blockages. Sharp, angular GH25 particles combined with rounder GP25 can form wedge-shaped plugs (“bridging”) in the hopper or at the discharge opening, especially under vibration or high humidity.
- Segregation (the “Brazil nut effect”). When shaken, sharp-edged GH25 particles may separate differently from the more rounded GP25. This creates zones with uneven concentrations of each grade and undermines process stability.
- Changing impact behaviour and intensity. GH25 keeps its sharp edges and acts more aggressively on the surface; GP25 cushions the impact more gently. In a mix, impacts become inconsistent – partly hard, partly soft – making blasting results harder to reproduce.
- Faster and uneven wear of nozzles and equipment. Harder GH25 particles wear nozzles, blast wheels and pipework more heavily; with a variable mix, wear becomes unpredictable.
- More dust. A mix with different microstructures (more brittle GH25 plus small fragments of softer GP25) can generate more fine dust than a single-grade abrasive. This requires tighter control of dust extraction and operator PPE.
- Corrosion. The risk of a chemical reaction between two steel abrasives is minimal, but the mix, like any steel grit, must stay dry. Moisture and acidic or alkaline contaminants accelerate corrosion of both the particles and the equipment.
How Mixing Affects Blasting Quality
Abrasive composition directly determines the material removal rate (MRR) and surface quality:
- Material removal rate. Thanks to its hardness and sharp edges, GH25 removes scale efficiently and delivers high productivity. GP25 is softer, and its effectiveness gradually drops as the particles round off. In a mix, performance falls somewhere in between and depends on the actual share of GH25, so for stable output the GH share must be kept strictly constant.
- Surface roughness. The more GH25 in the mix, the deeper and sharper the surface profile (beneficial for coating adhesion). A predominance of GP25 produces a smoother, less rough surface. Fluctuations in the ratio between abrasive batches lead to inconsistent roughness.
- Cleaning uniformity. Areas blasted mainly with GH25 will be cleaner and rougher than those where GP25 prevailed, reducing consistency within a single part or batch.
- Process repeatability. Even small changes in the GH25/GP25 ratio alter the final blasting parameters. If a process specification is designed for pure GH25 and GP25 ends up in the hopper, test results may fall outside specification.
If You Still Want to Test a Mix: Quality Control Protocol
If a company plans to test a GH25 + GP25 mix (e.g. 50:50 by weight), we recommend a series of trials following this procedure:
- Abrasive preparation – load the mix in the defined ratio and blend thoroughly until homogeneous; check dosing accuracy (± 2%) and absence of moisture.
- Equipment setup – set the working air pressure (e.g. 0.5–0.7 MPa), stand-off distance (≈ 300 mm), angle and feed mode according to the usual settings for the material.
- Blasting a test panel – blast a standard steel panel with a uniform layer of rust or mill scale for a set time; criterion: full surface coverage with no missed spots.
- Measuring material removal – weigh the panel before and after blasting and calculate MRR (g/min); the result must be within acceptable limits relative to a pure GH25 reference.
- Roughness assessment – measure Ra with a profilometer at several points; deviation from the target value max. ± 10%.
- Feed uniformity analysis – take abrasive samples from the hopper and from the collection bin after operation and verify (e.g. by hardness testing or particle analysis) that the GH25 share has not changed by more than 5% from the initial composition.
- Equipment wear assessment – compare the condition of the nozzle and internal parts before and after the test; criterion: wear within normal operating limits, with no unusual material loss.
- Documentation – record all parameters, mix formulation, settings and results in a test report; perform at least two repetitions for each abrasive configuration.
If the MRR, roughness or mix homogeneity results deviate significantly from requirements, the mix is considered unsuitable for production use.
Alternatives to Mixing GH25 and GP25
If testing shows that mixing reduces process stability, one of the following solutions is a better choice:
- Separate hoppers. Use GH25 and GP25 in different hoppers or feed lines and switch abrasives depending on the task – rough cleaning or finishing.
- Controlled dosing. An automatic feed system with two conveyors or screw feeders can dose two abrasives at a set ratio during the work cycle.
- Pre-blending under controlled conditions. If a stable mix is genuinely needed, a GH25 + GP25 batch can be pre-blended in a rotating drum, checked for homogeneity and only then loaded into the production hopper. This reduces the risk of uncontrolled segregation on the line.
- Compatible grades from one manufacturer. Instead of improvised GH25/GP25 mixing, consider abrasives with closer hardness and structure (e.g. GP with GL, or GH with GL), or ready-made blends developed by the supplier specifically for this purpose.
- Single-source purchasing. When GH25 and GP25 come from the same manufacturer using the same technology, they are more likely to be compatible in one process than batches of different origin.
Summary
GH25 and GP25 are chemically almost identical abrasives that differ fundamentally in hardness and in-service behaviour: GH25 stays sharp and aggressive throughout its life, while GP25 rounds off quickly and acts more gently. ISO 11124-3 and SAE J1993 do not formally prohibit mixing the two grades in one hopper, but they also give no guidance on doing it safely. In practice, mixing increases the risk of hopper blockages, uneven feed, faster nozzle wear and inconsistent surface quality. The final decision should therefore be based on your own trials and consultation with the blasting equipment manufacturer.
Ingritech supplies certified steel grit and steel shot in GH25 and GP25 grades from Ukraine and EU countries, delivered in separate batches matched to the specific process – heavy-duty cleaning, finishing profiles or combined applications. Need help choosing an abrasive for your equipment and surface type? Contact our team and we will help you select the optimal grade and size.
Frequently Asked Questions about GH25 and GP25
Can GH25 and GP25 be mixed in one hopper?
Formally yes – both abrasives are magnetic and meet the same standards (ISO 11124-3, SAE J1993). However, mixing without prior testing is not recommended due to the risk of hopper blockages, segregation and inconsistent blasting quality. Separate hoppers or controlled dosing are the safer options.
What is the main difference between GH25 and GP25?
The main difference is hardness and particle behaviour. GH25 has a hardness of 60–66 HRC and keeps its sharp edges in use, making it suitable for coarse profiles and scale removal. GP25 has 42–51 HRC and rounds off quickly during blasting, so it treats the surface more gently.
Which should I choose for blasting – GH25 or GP25?
For heavy-duty work such as deep cleaning, removing heavy mill scale or creating a coarse anchor profile for coatings, GH25 is the better choice. For general rust and scale removal without excessive damage to the base material, the softer and tougher GP25 is more suitable.
Do GH25 and GP25 have the same size?
Yes, both grades are produced in G25 size according to SAE J444, with a nominal particle size of approx. 0.8–1.2 mm. They differ only in hardness and particle behaviour during operation, not in size.